What Is a Ceramic Fiber Spinning Machine?
A ceramic fiber spinning machine — also called a fiberizer or centrifugal fiberizing machine — is the equipment that converts molten aluminosilicate glass into fine ceramic fibers. It sits directly downstream of the melting furnace and is arguably the single most important machine in a ceramic fiber blanket production line.
The quality of the fiber it produces determines everything downstream: blanket strength, thermal conductivity, shot content, and ultimately whether the finished product meets specification. A poorly designed spinning machine cannot be compensated for by better needling or packaging. The fiber quality is set here.
How It Works
The operating principle is straightforward in concept but demanding in execution. A thin stream of molten glass — at 1800°C to 2200°C depending on composition — flows from the furnace discharge spout and falls by gravity onto a set of high-speed spinning wheels.
The wheels are arranged in a cascading configuration. The first wheel receives the molten stream and flings it outward by centrifugal force. The material transfers to the second wheel, then the third, and in some designs a fourth. Each successive wheel spins faster than the previous one, progressively attenuating the material into finer and finer filaments.
The centrifugal force overcomes the surface tension and viscosity of the molten glass, drawing it into fibers with diameters in the range of 2 to 5 micrometers. Simultaneously, a controlled air stream around the wheel assembly helps carry the formed fibers away toward the collection conveyor while also cooling them rapidly to solidify their amorphous structure.
Material that fails to fiberize — droplets that are too large or cool too quickly — becomes "shot." These are small, hard, non-fibrous particles that degrade blanket quality. Minimizing shot is a primary goal of spinning machine design.
Spinning vs Blowing: Pros and Cons
The two main fiberization methods in ceramic fiber production are spinning and blowing. Each has advantages:
Spinning (centrifugal method):
- Produces longer fibers with better length-to-diameter ratio
- Lower shot content — typically 8% to 15%
- More uniform fiber diameter distribution
- Better suited for blanket and board products requiring mechanical strength
- Lower energy consumption per ton of fiber produced
- Higher capital cost for the machine itself
Blowing (air-jet or steam-jet method):
- Simpler machine design with lower capital cost
- Can produce very fine fibers (below 2 micrometers)
- Higher shot content — often 20% to 40%
- Shorter fiber length, less suitable for needled products
- Higher energy consumption due to compressed air or steam requirements
- Better suited for loose-fill insulation and wet-felt processes
For blanket production lines, spinning is the industry standard. The longer fibers interlock better during needle punching, producing blankets with higher tensile strength and better resilience after compression.
Key Parameters
Fiber quality from a spinning machine depends on several tightly controlled parameters:
Wheel speed: The rotational speed of each wheel determines the centrifugal force applied to the molten material. Typical speeds range from 6,000 RPM on the first wheel to 12,000 RPM or higher on the final wheel. Higher speeds produce finer fibers but also increase shot if the melt viscosity is not matched correctly.
Melt temperature and viscosity: The glass must be at the right viscosity when it reaches the wheels. Too viscous (too cool), and it forms thick fibers and excessive shot. Too fluid (too hot), and it splatters rather than drawing into filaments. The target viscosity window is typically 10 to 100 Pascal-seconds at the fiberizing point.
Gap settings: The distance between wheels and between the spout and the first wheel affects how material transfers between stages. Gaps that are too large cause material to cool and form shot. Gaps that are too small create turbulence and uneven fiber distribution.
Air flow: The velocity and direction of the assist air around the wheel assembly controls fiber trajectory and cooling rate. Proper air flow carries fibers to the collection belt in a uniform cloud while preventing re-entrainment of shot particles.
Fiber Quality Metrics
The spinning machine's performance is judged by measurable fiber characteristics:
- Fiber diameter: Target range is 2 to 5 micrometers. Fibers below 2 micrometers are fragile and create dust. Fibers above 5 micrometers reduce insulation performance and create a harsh hand feel.
- Shot content: The weight percentage of non-fibrous particles larger than 0.25 mm. Quality blanket production requires shot content below 15%. Premium lines achieve below 10%.
- Bulk density of raw cotton: The as-formed fiber mat should have a consistent bulk density — typically 80 to 120 kg/m3 before needling. Inconsistency here translates directly to density variation in the finished blanket.
- Fiber length: Longer fibers (average above 100 mm) produce stronger blankets. Spinning machines that generate excessive short fibers create weak spots in the web.
How Spinning Affects the Final Product
The fiber produced by the spinning machine propagates its quality through every subsequent process:
Blanket tensile strength depends directly on fiber length and the degree of interlocking achieved during needle punching. Longer, more uniform fibers create more interlock points per unit volume, resulting in higher strength. Short fibers and excessive shot create weak planes where the blanket tears.
Thermal conductivity is influenced by fiber diameter. Finer fibers create more air pockets per unit volume, reducing convective heat transfer within the blanket structure. A blanket made from 3-micrometer fibers will have measurably lower thermal conductivity than one made from 5-micrometer fibers at the same density.
Compression recovery — the ability to spring back after being compressed during shipping — depends on fiber resilience. Fibers with consistent diameter and minimal micro-cracks recover better. Overheated or chemically inhomogeneous fibers become brittle and break during compression, leading to permanent thickness loss.
Jinyuan's Spinning Technology
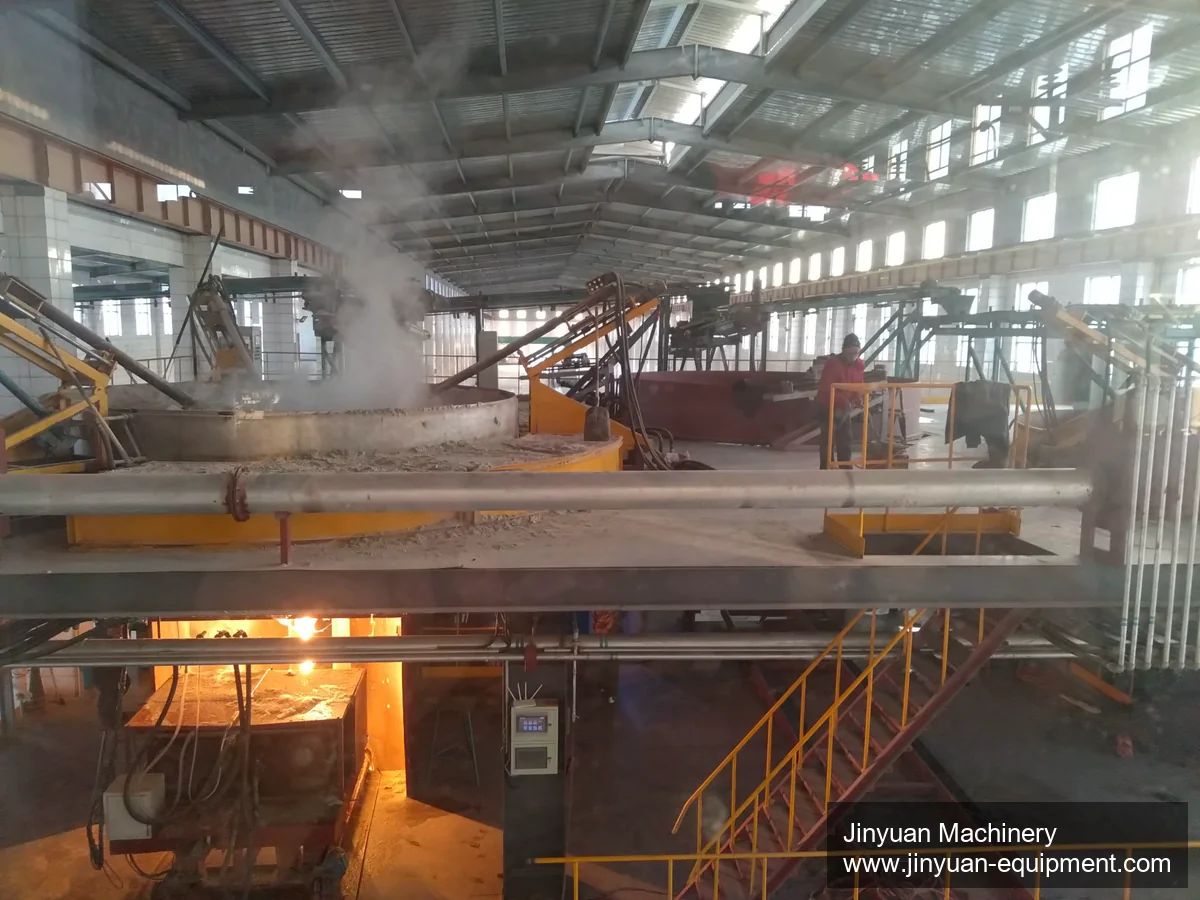
Jinyuan's spinning machines use a high-speed four-wheel design that maximizes fiber quality while maintaining production throughput. Key features include:
- Four-wheel cascade configuration — progressive speed increase from wheel one through wheel four for optimal fiber attenuation
- Independent frequency drives — each wheel has its own VFD, allowing precise speed adjustment without affecting other wheels
- Water-cooled bearings — the wheel shafts operate in an environment radiating heat from 1800°C melt; water-cooled bearing housings maintain bearing temperature below 80°C for extended service life
- Quick-change wheel design — wheels can be replaced in under thirty minutes without removing the drive assembly, minimizing downtime
- Adjustable air nozzles — multi-zone air assist with individually adjustable nozzles for tuning fiber trajectory to match different product grades
- Nitrogen-protected spout interface — prevents oxidation of the molybdenum discharge components and ensures consistent melt flow geometry
The result is fiber with average diameter of 3 to 4 micrometers, shot content consistently below 12%, and fiber length distribution optimized for high-strength needle-punched blankets.
Maintenance Tips
Spinning machines operate in extreme conditions. Proper maintenance keeps fiber quality consistent and prevents unplanned shutdowns:
- Inspect wheels daily — look for erosion, cracks, or buildup of solidified material on wheel surfaces. Even minor surface damage disrupts fiber formation and increases shot.
- Check bearing temperature — monitor cooling water flow rate and outlet temperature. A rise in bearing temperature indicates reduced cooling efficiency or bearing wear.
- Clean air nozzles weekly — fiber dust accumulates on nozzle surfaces and disrupts airflow patterns. Blocked nozzles cause uneven fiber distribution across the web width.
- Verify wheel alignment monthly — thermal cycling can shift wheel positions. Misaligned wheels cause material to miss the next stage, creating excessive shot and reducing yield.
- Replace wheels on schedule — even with careful operation, wheel surfaces erode over time. Track running hours and replace before quality degrades. Typical wheel life is 200 to 500 hours depending on melt chemistry.
- Inspect the spout regularly — erosion of the molybdenum spout changes the melt stream geometry. A worn spout produces an uneven stream that overloads one side of the first wheel.
Talk to Our Engineers
The spinning machine is the heart of your ceramic fiber blanket production line. Getting it right determines whether your blankets meet market specifications or end up as seconds.
Jinyuan's engineers have decades of combined experience in fiberizing technology. Whether you are planning a new line or upgrading an existing fiberizer, we can help you select the right configuration for your product mix and capacity targets.
Contact us to discuss your fiberizing requirements. We will provide technical specifications, reference projects, and a detailed proposal tailored to your needs.
Related Reading
Continue with these guides and equipment pages: